I hear it at almost every conference and trade show. “We tried oil mist lubrication once. It didn’t work here.” I take that statement seriously. The people who say it usually watched a real system struggle. They saw plugged reclassifiers, hot bearings, oily equipment and mist drifting across the unit. Those problems were real.
But here is the puzzle. Oil mist has been protecting process pumps in U.S. refineries for decades, with typical pump MTBF of 4 to 6 years. Best-practice facilities have >10-year MTBF! The same technology that failed in one plant is delivering outstanding results in the plant down the road.
So what is the difference? In my experience, it is almost never the technology. It is how the system was designed, how it was installed, and, most of all, how well the people around it were trained and supported over time.
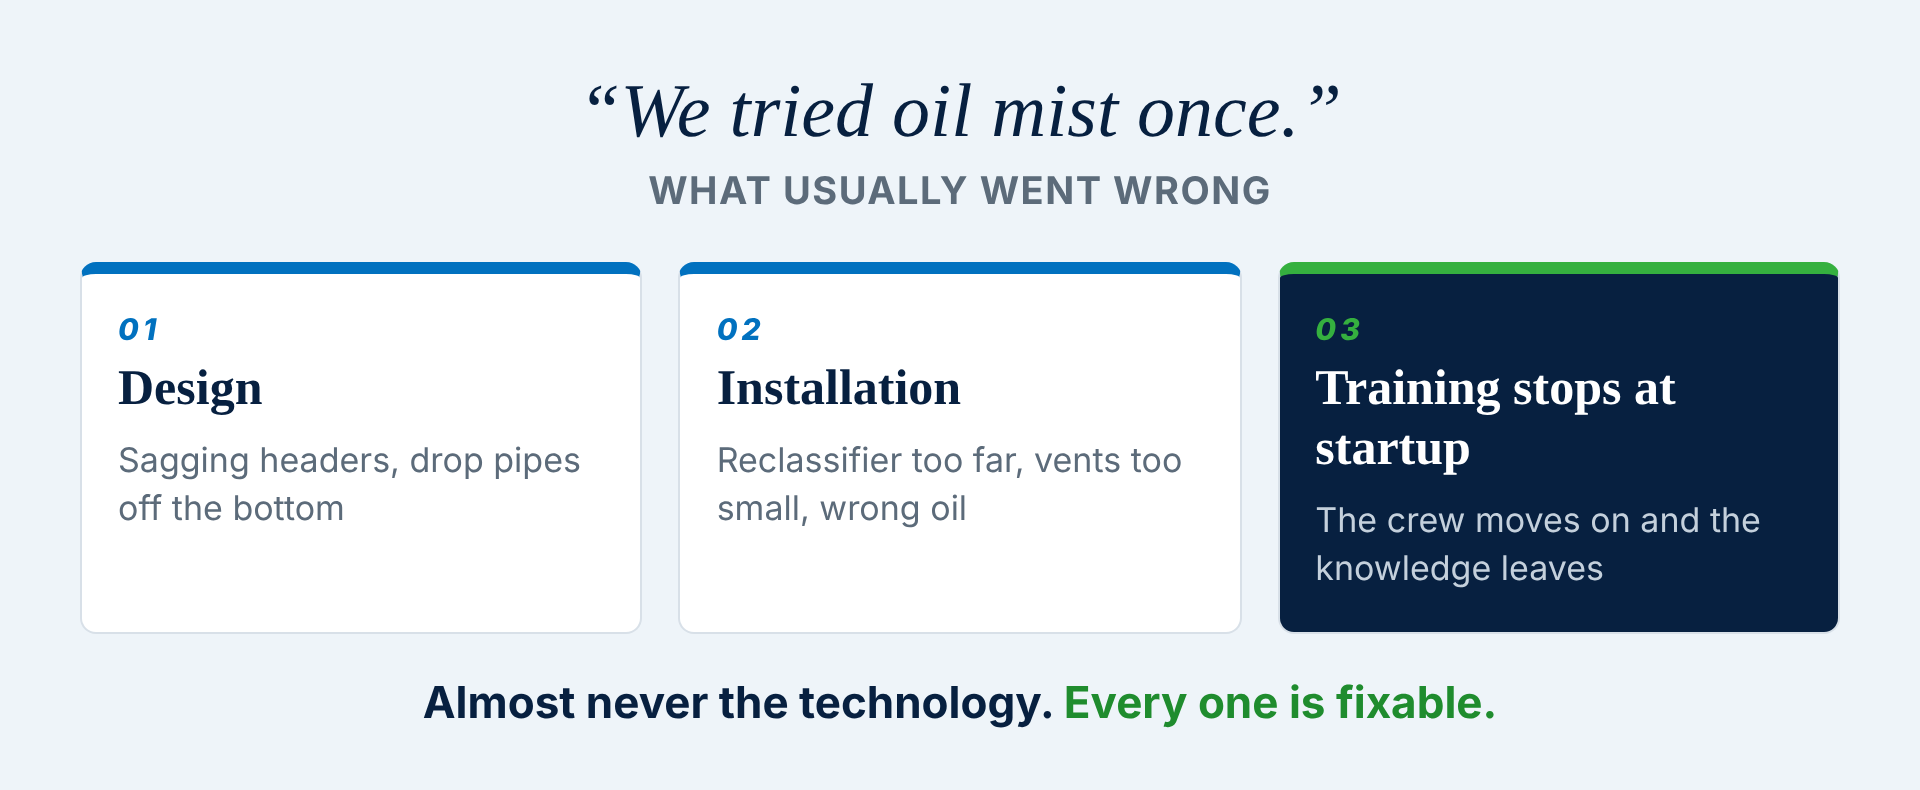
What Usually Went Wrong: Design and Installation
Charles Towne made this point decades ago. Most of the early failures blamed on oil mist came from distribution design, not from the technology itself. The same mistakes still show up in the field today:
- Sagging or poorly sloped headers. Headers must slope continuously so condensed oil drains back toward the generator or a drain leg. A sag creates a low spot where oil pools and blocks the mist.
- Drop pipes taken off the bottom of the header. Drop pipes belong on the top of the header. A bottom connection collects liquid oil instead of mist and sends it to the wrong place, creating a housekeeping problem.
- Reclassifiers in the wrong place. Place the reclassifier within 6.6 feet (2 meters) of the bearing. Beyond that, the oil particles fall out of the mist before they arrive.
- Undersized vents and drains. Size the vent and drain 3 to 4 times the reclassifier orifice. An undersized vent creates back-pressure, restricts mist flow, and can cause a false-high oil level reading while the bearing starves.
- The wrong oil. Use paraffin-free oil only. Paraffin wax can precipitate during temperature swings and plug every reclassifier in the system. Because oil mist lubrication drastically reduces oil usage, many customers can now justify moving to a premium synthetic.
Every one of these is fixable. None of them is a reason to abandon the technology.
Clearing Up a Few Common Misunderstandings
Some of the resistance to oil mist comes from ideas that have been passed along for years. A few deserve a fresh look:
- “Oil mist is maintenance-free.” It is not, and nobody who knows the technology claims it is. It needs very little maintenance, but it does need some: a few minutes on the daily operator round and routine service by trained technicians. “Set and forget” is where many systems start to fail.
- “Oil mist will fix our bearing problems.” It will prevent many of them, but it cannot repair a bearing that is already damaged. If a bearing fails shortly after a conversion to pure oil mist, it was likely compromised before the conversion.
- “Oil mist is an environmental problem.” Visible stray mist is a symptom, not a normal condition. It points to a vent, drain, or sizing issue. Closed-loop systems can recover up to 99% of the oil and are recognized as Best Available Technology for process equipment lubrication. All oil mist generators should be calibrated to the oil!
- “It didn’t work here, so it doesn’t work.” A failed installation tells you something about that installation. It does not tell you much about the technology.
The Real Root Cause: Training That Stops at Startup
Here is the pattern I see most often. A new oil mist system is installed. The vendor commissions it and trains the crew that is on site that week. Everyone understands the system. It runs well.
Then time passes. Operators rotate. Mechanics retire. Contractors change. Engineers move to other units or other companies. Five years later, almost nobody in the plant was in that original training room. The knowledge left with the people who had it.
Now the reclassifiers get swapped for whatever is in the storeroom. A pump comes back from the shop with its drain-back port open. A new pump is tied into the header without anyone checking generator capacity. Nobody recognizes the early warning signs, so small problems become bearing failures. Eventually someone concludes that oil mist “doesn’t work here,” and the system is removed.
I have seen this happen at major facilities, both overseas and right here on the Gulf Coast. In each case the systems were pulled out, not because the technology failed, but because the knowledge to run them was never kept alive.
Training is not an event. It is a habit. One-time training at startup is not enough for any reliability program, and oil mist is no exception.
Continuous Training for Every Role
Oil mist touches many people in a plant, and each one needs to understand their part. Continuous training means regular refreshers, onboarding for every new hire, and updates whenever the system changes.
- Operators. The daily round takes only a few minutes. Operators need to know what normal looks like, what abnormal looks like, how to refill the reservoir without contaminating it, and how to respond to an alarm.
- Mechanics and maintenance technicians. They need to understand how mist is generated and distributed, how to service reclassifiers and fittings, and how to troubleshoot a problem to its root cause instead of just swapping parts.
- Shop personnel. This group is often forgotten. When a pump or motor goes to the shop, it must come back set up for oil mist: correct fittings, drain-back ports plugged, the right reclassifiers, and no grease packed into a motor that has been converted to mist.
- Engineers. Reliability and project engineers need to know design and specification basics, API-610 dual-injection requirements, generator sizing, and how to handle oil mist in the management of change process so the system is not quietly overloaded or bypassed.
- Management. Leaders do not need to service a reclassifier. They do need to understand what the system delivers, what it costs to support, and why training budgets and staffing directly affect equipment reliability.
Building a Culture of Reliability
Training by itself is not the whole answer. The plants that succeed with oil mist treat it as a reliability system, not a utility. A few habits set them apart:
- Someone owns it. A named system owner or champion is responsible for the health of the oil mist system and the knowledge around it.
- It lives in the CMMS. Inspections, reclassifier service, and generator checks are scheduled work, not tasks that happen when someone remembers.
- It is part of management of change. Adding equipment, modifying piping, or changing oils triggers a review.
- Procedures are written down. Clear, current procedures mean the next crew does the job the same way as the last one.
- Results are measured. Bearing temperatures, MTBF, and failure data show whether the system is performing, and they give management a reason to keep supporting it.
- Knowledge is shared. Lessons from failures and successes are passed along instead of leaving with the person who learned them.
How to Take a Second Look
If your plant tried oil mist before, or if your current system is struggling, here is a practical place to start:
- Start at the oil mist generator. Survey the existing or former system against API standards and industry best practices.
- Correct the distribution design: header slope, drop pipes, reclassifier placement, and vent and drain sizing.
- Verify the oil type and viscosity.
- Name a system owner.
- Train every role, then schedule the next round of training before this one ends.
- Track bearing temperatures and MTBF so the results speak for themselves.
Conclusion
When someone tells me oil mist didn’t work at their facility, I believe them. I also believe it can. The technology has a long and well-documented track record. What makes the difference is the design, the installation, and a workforce that keeps its knowledge current long after the startup crew has moved on. Build that culture, and oil mist delivers the results it was designed to deliver.
If your plant is taking a second look at oil mist, I am always happy to talk it through. Feel free to reach out.
Sources and Further Reading
- Towne, C. (1994). Oil Mist Lubrication for the Petrochemical Industry — Texas A&M Turbomachinery Laboratories
- Ehlert, D. Getting the Facts on Oil Mist Lubrication — Texas A&M Turbomachinery Laboratory
- Guidelines for Oil Mist Lubrication — Machinery Lubrication
- Bloch, H.P. & Rehman, C. Oil Mist Lubrication for Pumps and Electric Motors — Machinery Lubrication
- Bloch, H.P. & Shamim, A. Oil Mist Lubrication: Practical Applications. Fairmont Press.